Technology
Common PCBA Defects and How to Prevent Them
Tombstoning, bridging, cold joints, voiding — learn what causes the seven most common PCBA defects and how DFM, SPI, and AOI prevent them before production.
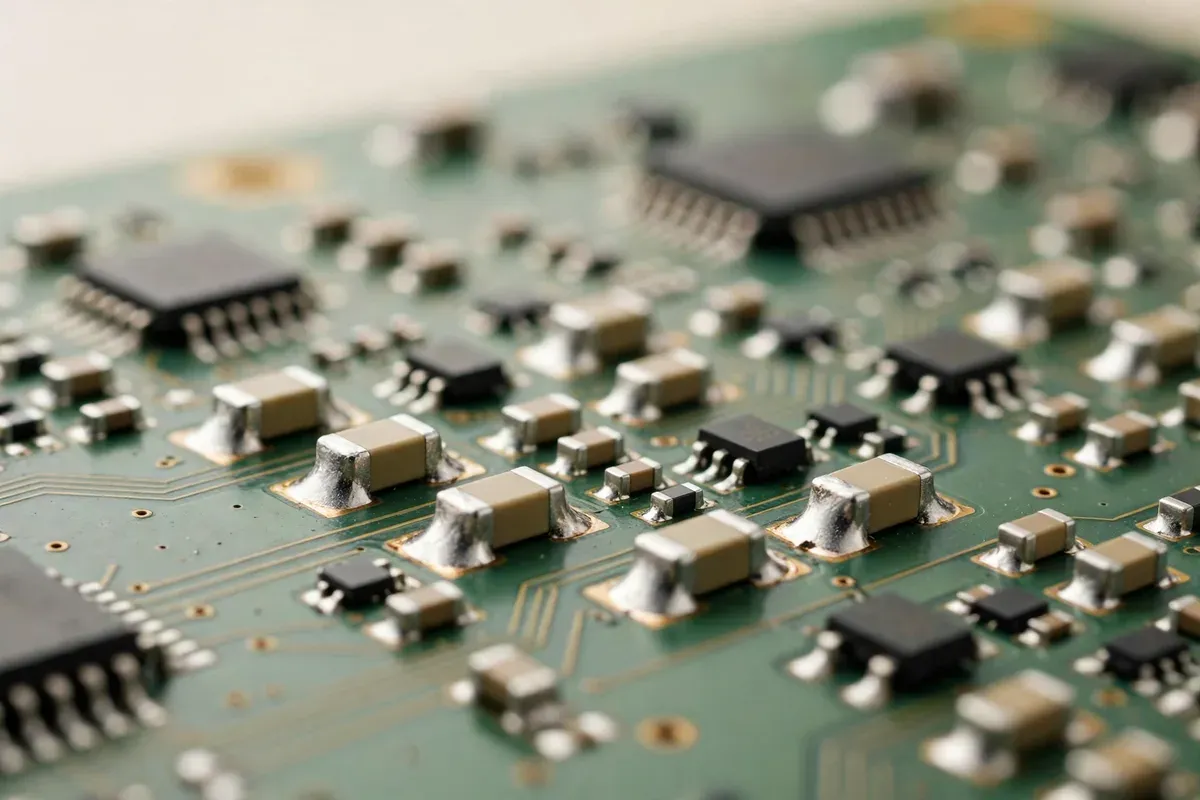
Most PCBA defects are not random accidents.
They are predictable outcomes of design choices, process settings, and material handling. The same seven defects appear in factory after factory.
Most of them are preventable, and the earlier a risk is found, the cheaper it is to fix. A pad layout fixed during design costs almost nothing. The same defect found after mass production costs rework, scrap, and delayed shipments.
This guide covers the seven most common PCBA defects, their causes, and how to prevent them.
1. Tombstoning
A small chip component stands upright on one end during reflow, like a tombstone. One joint is missing entirely, and the board fails electrical testing.
It happens when the paste on one pad melts before the other, and surface tension pulls the lighter end upward. Small parts such as 0201 and 0402 components are the most vulnerable.
Common causes include:
- Unequal or asymmetric pad design
- One pad tied to a large copper plane, which heats more slowly
- Uneven solder paste volume between the two pads
- A reflow ramp rate that is too fast
Prevention starts with symmetric pad design, balanced thermal connections, matched paste volume on both ends, and a reflow profile that heats the board evenly.
2. Solder Bridging
A solder bridge is an unintended connection between adjacent pads or leads. It creates a short circuit and is a common cause of failure at testing.
Bridging is usually a paste problem: too much paste, a misaligned stencil, or apertures too large for fine-pitch parts all leave excess solder between pads. Once it melts, surface tension pulls the excess into a bridge.
To prevent bridging:
- Size stencil apertures for the pitch, reducing aperture area on fine-pitch parts
- Check stencil alignment and gasketing before printing
- Inspect paste deposits with SPI before placement
- Keep adequate pad spacing in the layout, especially under QFP and QFN packages
3. Cold Solder Joints
A cold solder joint looks dull, grainy, and rough instead of smooth and shiny. The solder never fully melted or wetted the surfaces properly, leaving a weak connection that can fail under thermal cycling or vibration.
The most common cause is a reflow profile that delivers too little heat: a peak temperature too low or too little time above liquidus. Other causes include oxidized pads or leads, contaminated surfaces, and large ground planes that draw heat away from the joint.
Prevention means a reflow profile matched to the paste specification, clean surfaces, and thermal relief design that lets pads heat evenly.
4. Solder Voiding
Voids are gas bubbles trapped inside a solder joint. They are invisible from the surface and mostly affect BGA and QFN packages, where large joints hide them from inspection. Large voids weaken the joint and reduce thermal conductivity.
Voids form when gases from flux volatiles, moisture, or outgassing cannot escape before the solder solidifies. Skipping the bake on moisture-sensitive parts, vias under pads, and short soak profiles all increase voiding.
To reduce voiding:
- Bake moisture-sensitive parts and PCBs per their MSL rating
- Fill and cap vias under BGA and QFN pads
- Allow an adequate soak so gases escape before peak temperature
- Select a low-voiding paste for sensitive designs
- Verify with X-ray inspection, since AOI cannot see inside a joint
5. Insufficient Solder
Insufficient solder leaves thin, weak joints, or open connections where solder never reaches the lead. The board may pass a functional test and fail later in the field.
The root cause is usually at printing: apertures that are too small, paste that fails to release, or a worn stencil.
Prevention starts with correct aperture sizing and regular stencil cleaning. SPI catches low paste volume before placement, when the fix costs only a reprint. Check for pad oxidation too: oxidized surfaces resist wetting even when paste volume is correct.
6. Component Shift and Skew
A correctly placed component can still move during reflow. It ends up shifted or rotated off its pads, creating weak joints on one side and possible bridging on the other.
Uneven paste deposits are the usual cause: when one pad has more paste, surface tension pulls the component toward the larger deposit as the solder melts. Placement errors and board warpage add to the problem.
Prevention depends on consistent paste volume and accurate placement. Fiducial marks help the placement machine locate the board precisely. Symmetric pads also help: when both pads melt evenly, surface tension pulls the component back to center.
7. Solder Balls
Solder balls are small spheres of solder scattered across the board, away from the joints. They can lodge under components, cause intermittent shorts, and fail cleanliness requirements.
They form when excess paste or slump leaves solder outside the pad area, or when moisture in the paste turns to steam during reflow and spatters droplets. A fast ramp makes spattering worse.
To prevent solder balls:
- Store and handle paste correctly, and respect its shelf life and floor life
- Avoid excess paste volume and slump through correct stencil design
- Use a controlled reflow ramp rate
Prevention Is a Process, Not a Single Step
No single check catches every defect. Prevention works in layers, and each layer is cheaper than the next.
DFM comes first. A review before fabrication checks pad geometry, spacing, thermal relief, stencil apertures, and test access. Most defects in this guide trace back to layout decisions.
SPI comes next. Solder paste inspection measures paste volume, height, and alignment before placement. Printing causes a large share of assembly defects, and SPI catches them when the fix is still a simple reprint.
AOI comes after reflow. Automated optical inspection checks every joint for bridging, tombstoning, shift, missing parts, and insufficient solder. X-ray adds coverage for hidden joints under BGA and QFN packages, where voiding hides.
Each inspection step costs far less than rework. Rework costs far less than a field failure.
Free DFM Review Before Manufacturing
Every defect in this guide is cheaper to prevent than to repair.
A professional DFM review finds the risks while changes are still inexpensive: pads that invite tombstoning, spacing that invites bridging, thermal layouts that invite cold joints.
Our engineering team provides a comprehensive DFM analysis before PCB fabrication and PCBA assembly. The review covers manufacturability, assembly feasibility, process compatibility, and potential reliability risks.
You receive practical engineering feedback instead of generic design comments.
No obligation.
No hidden fees.
If your PCB design is preparing for prototype or mass production, send us your Gerber files and BOM. Our engineers will perform a free DFM review and help identify manufacturing risks before they become production losses.